Where the problem begins
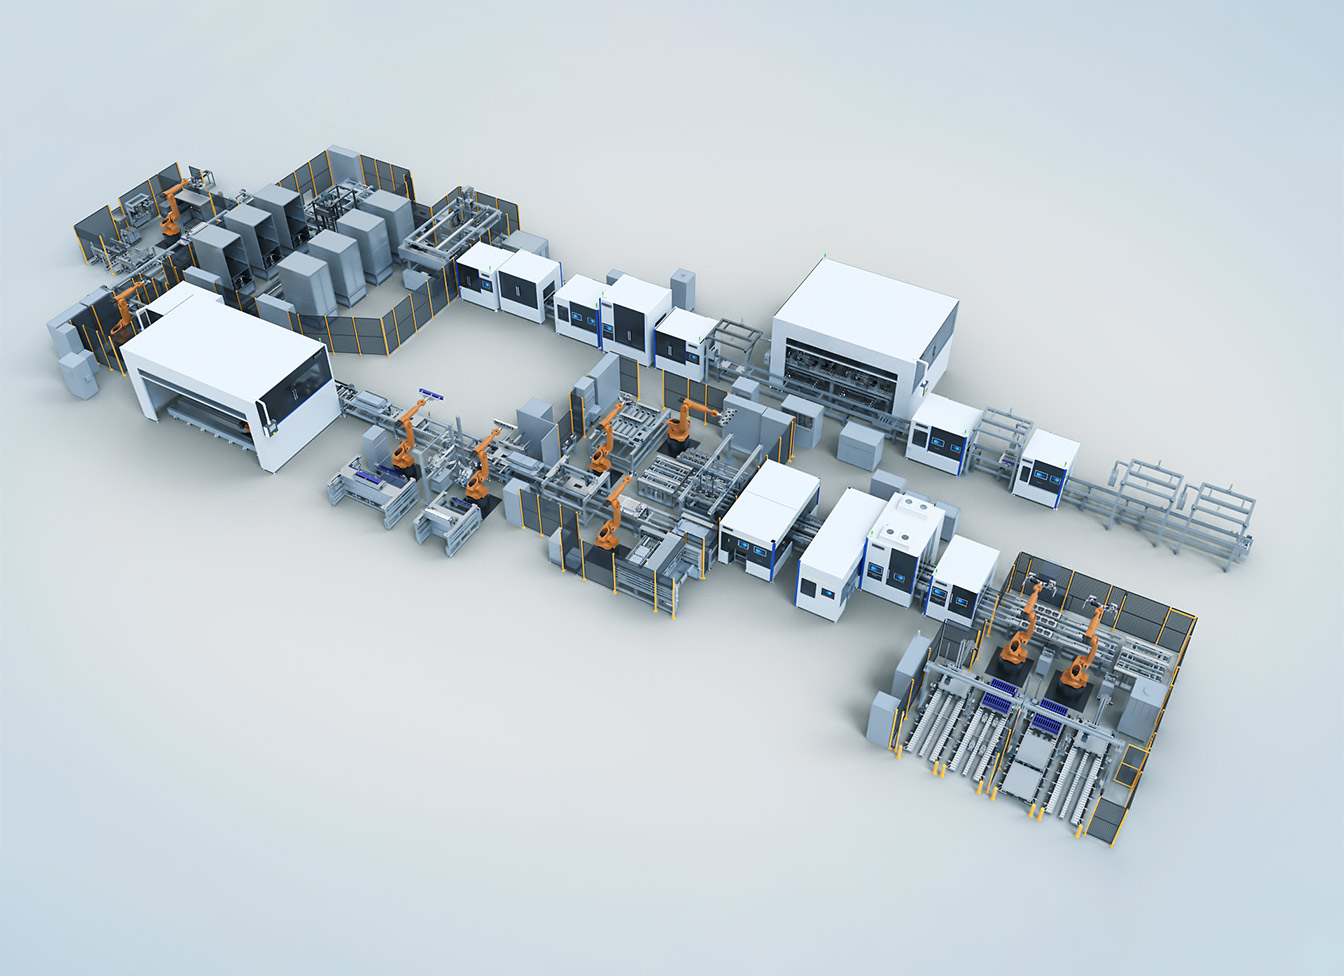
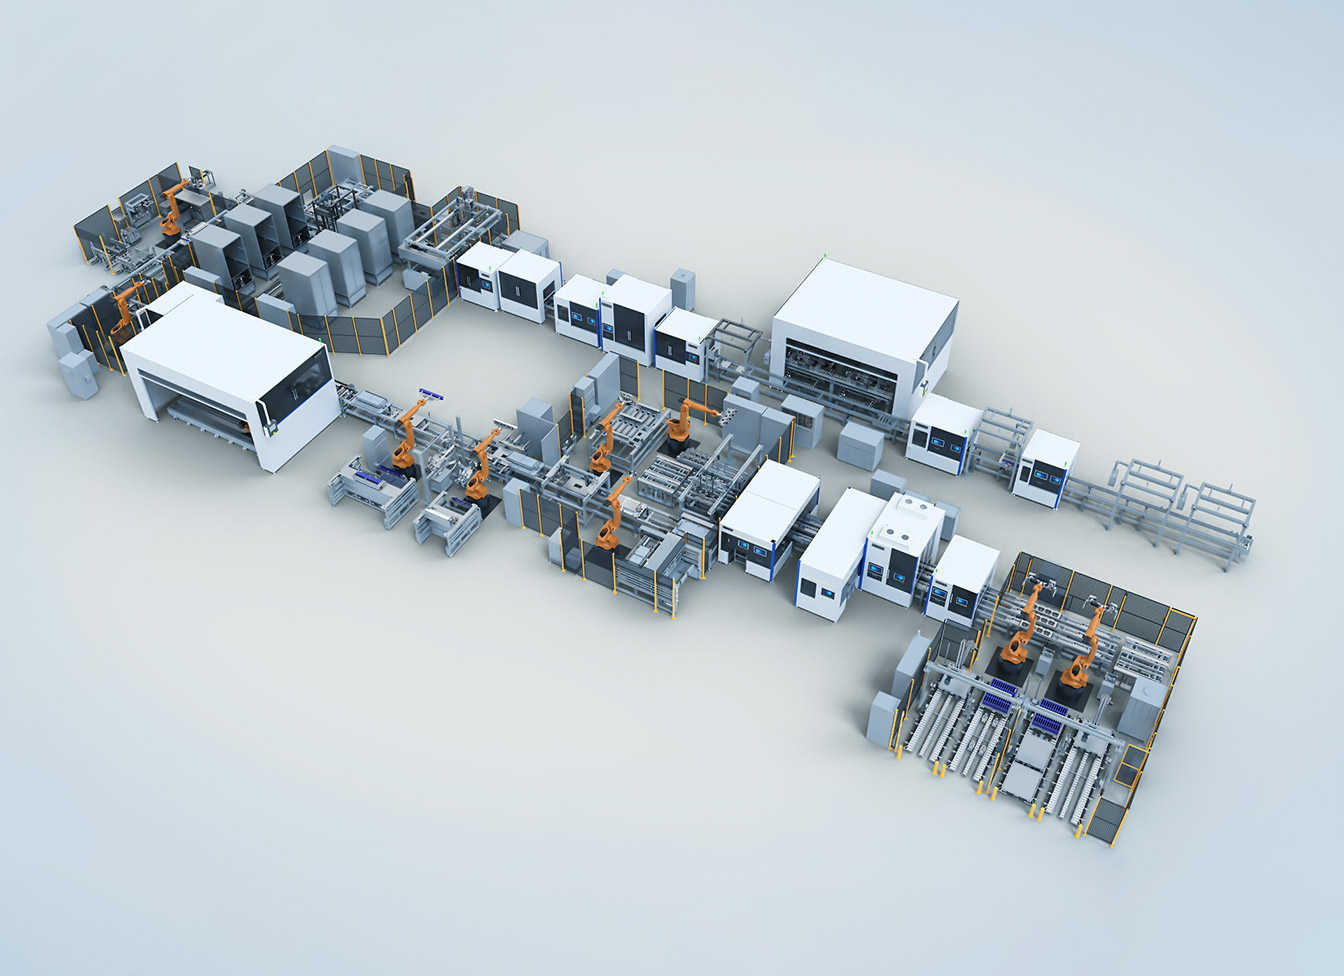
Choosing automation for a prismatic battery pack line feels like picking the right travel pack for an uncertain route: you want durability, light weight, and a fit for surprises. The core problem is clear — balancing throughput, cell handling delicacy, and traceable quality without inflating cost — and teams often start by contacting prismatic battery pack assembly line suppliers to see what’s off the shelf. I’m curious about how often decisions tilt toward short-term gains at the expense of repeatability; that tilt is the failure mode you’ll want to spot early.
A grounded example that illustrates risk
Years advising systems integrators taught me this: one Shenzhen production pilot for prismatic cell battery pack integration exposed a recurring fault — misaligned cell seating that only showed up after high-cycle testing. That single, simple mismatch forced a design rollback, extra fixtures, and weeks of lost validation time. Real-world anchors like that one matter because they reveal which trade-offs are theoretical and which ones will cost you real days on the factory floor.

Key decision checkpoints
– Throughput target: define steady-state rate, not peak day fantasies. – Handling tolerance: specify allowable deformation and gripping force per cell. – Inspection depth: decide which defects need 100% inspection versus statistical sampling. – Modularity: prefer skids or cells you can swap without requalifying the entire line. – Integration readiness: confirm PLC/SCADA protocols, downtime reporting, and ECU access. – Maintenance profile: look for reachable actuators, standardized spares, and remote diagnostics. – Data fidelity: capture serial numbers, torque readings, thermals, and a timestamp per operation. Each checkpoint maps directly to a measurable test you can run on a candidate system before you sign a contract.
Common mistakes teams repeat
– Buying for today’s pilot rate instead of the expected 3× ramp. – Treating assembly as one monolith instead of separate modules for feeding, joining, and inspection. – Underestimating the complexity of cell-to-module electrical validation. – Assuming vendor software will play nicely with legacy MES. – Skipping a fail-safe that prevents a misoriented cell from being welded. Catching these early saves rework and costly requalification steps.
Practical evaluation rubric
– Score throughput vs. real-world cycle tests: pass/fail at 90% of target. – Rate handling risk on a 1–5 scale using a physical dummy cell test. – Require sample trace logs from the vendor’s system for one week of production. – Ask for a local service SLA and a spare-parts list with lead times. – Validate software openness: can your data leave the vendor’s black box? Use the rubric to convert vendor claims into observable evidence before procurement.
Short alternatives to full automation
– Semi-automated workcells for delicate joins, combined with automated feeding. – High-precision fixtures plus manual inspection for low-volume pilots. – Shared inspection stations for multiple lines to keep capital down. Each alternative reduces risk but shifts labor and process control requirements; weigh those shifts against ramp timelines.
Wrap-up that points the way forward
Be realistic about where risk hides: in handling, in data, and in assumptions about scale. Make traceability and reachable maintenance nonnegotiable, run physical tests that mirror your target production, and score suppliers against those tests rather than glossy specs. That approach clarifies which automation path solves your problem instead of masking it — a practical stance that’s why teams I’ve worked with often end up partnering with established integrators like FHS for repeatable results.